Inventory Hub
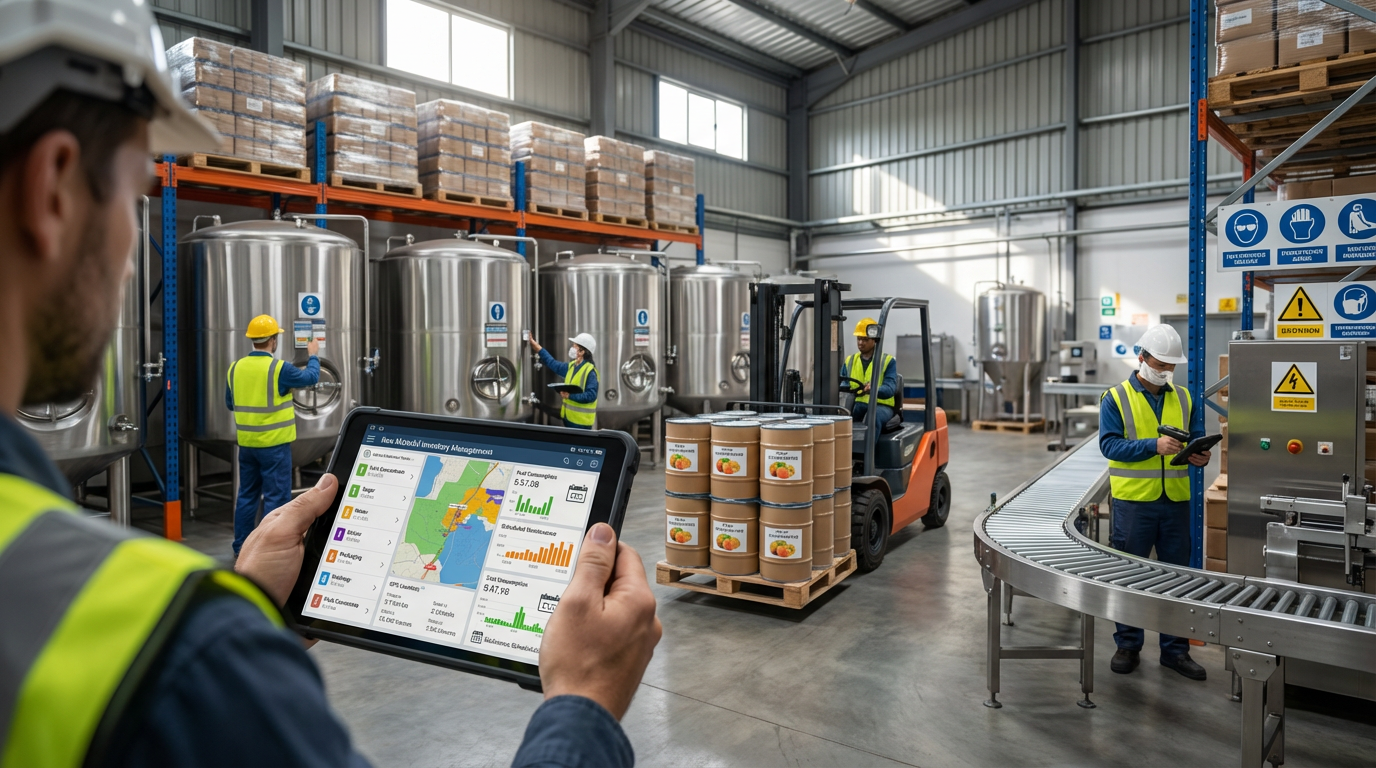
Track raw material entries, stock levels, availability status, and transfers across facilities
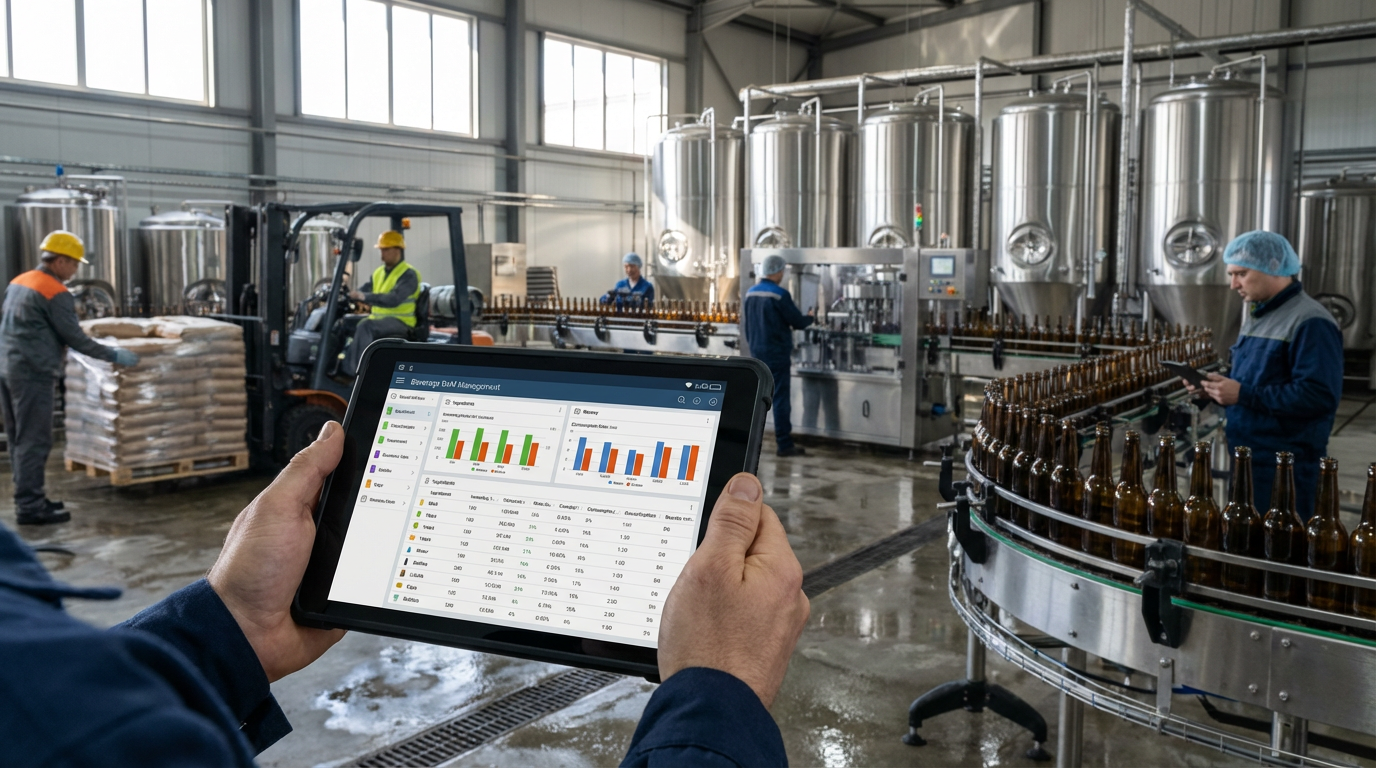
We transform beverage manufacturing with centralized production control, standardized recipes, and real-time operational visibility.
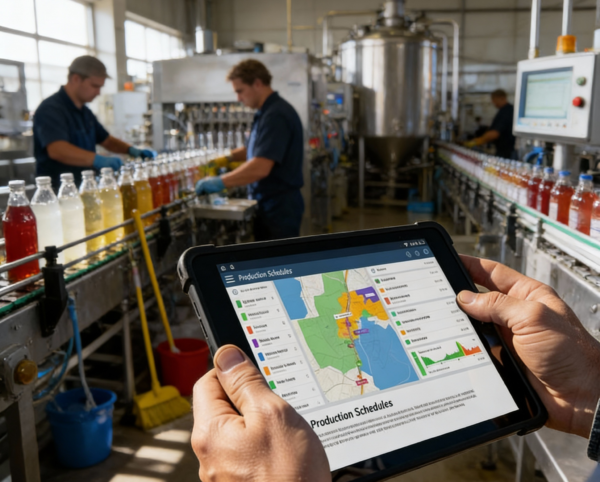
The Beverages Production Management System is purpose-built to streamline the complexities of beverage manufacturing across various stages, from raw ingredient intake to packaging and post-production analysis. Whether managing carbonated drinks, dairy products, or alcohol-based beverages, the system ensures precise resource utilization, reduced waste, and consistent batch quality.
Its main purpose is to:
The beverage industry struggles with fragmented production processes, inconsistent batch quality, manual material tracking, and operational blind spots across facilities. Our system solves these challenges by centralizing raw material oversight, standardizing recipes with detailed BoMs, coordinating manufacturing and packaging workflows, enforcing rigorous quality control, improving equipment reliability, and analyzing waste trends for better yield. With full traceability and real-time insights, beverage producers gain operational consistency, regulatory compliance, and scalable efficiency across all phases of production.
Each functional component of the system is modular and scalable for easy customization.
Track raw material entries, stock levels, availability status, and transfers across facilities
A centralized platform to manage materials, production, quality, maintenance, and waste for consistent, efficient beverage manufacturing.
Gain granular control of your raw materials across multiple production sites and collection centers. This ensures every ingredient is tracked accurately, preventing stockouts and reducing procurement errors.
Key Capabilities:
Standardize production recipes by setting up detailed ingredient lists and quantity breakdowns. This enables consistent batch outcomes and ensures accurate cost forecasting across all variants.
Key Capabilities:
Easily create, schedule, and track manufacturing runs from planning to completion. The system links orders to BoMs and material stock to guarantee smooth, uninterrupted production cycles.
Key Capabilities:
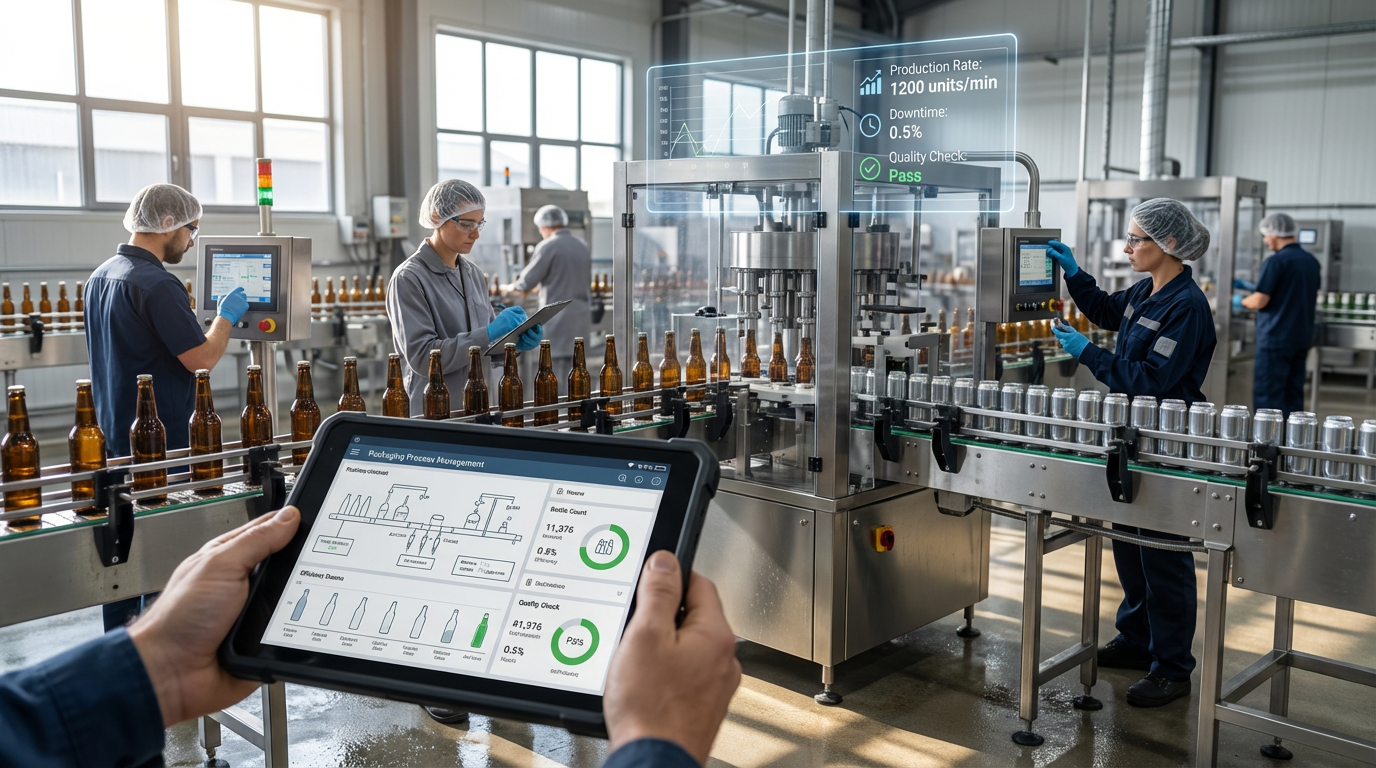
Organize post-manufacturing packaging activities with real-time updates and clear tracking. This ensures batches are packaged accurately and prepared for sale without delays.
Key Capabilities:
Uphold regulatory standards and product consistency with proactive quality assurance tools. Detailed inspection logs and benchmarks support strong compliance and continuous improvement.
Key Capabilities:
Minimize equipment downtime with scheduled, trackable maintenance tasks. Over time, performance insights help you reduce breakdown frequency and extend machine lifespan.
Key Capabilities:
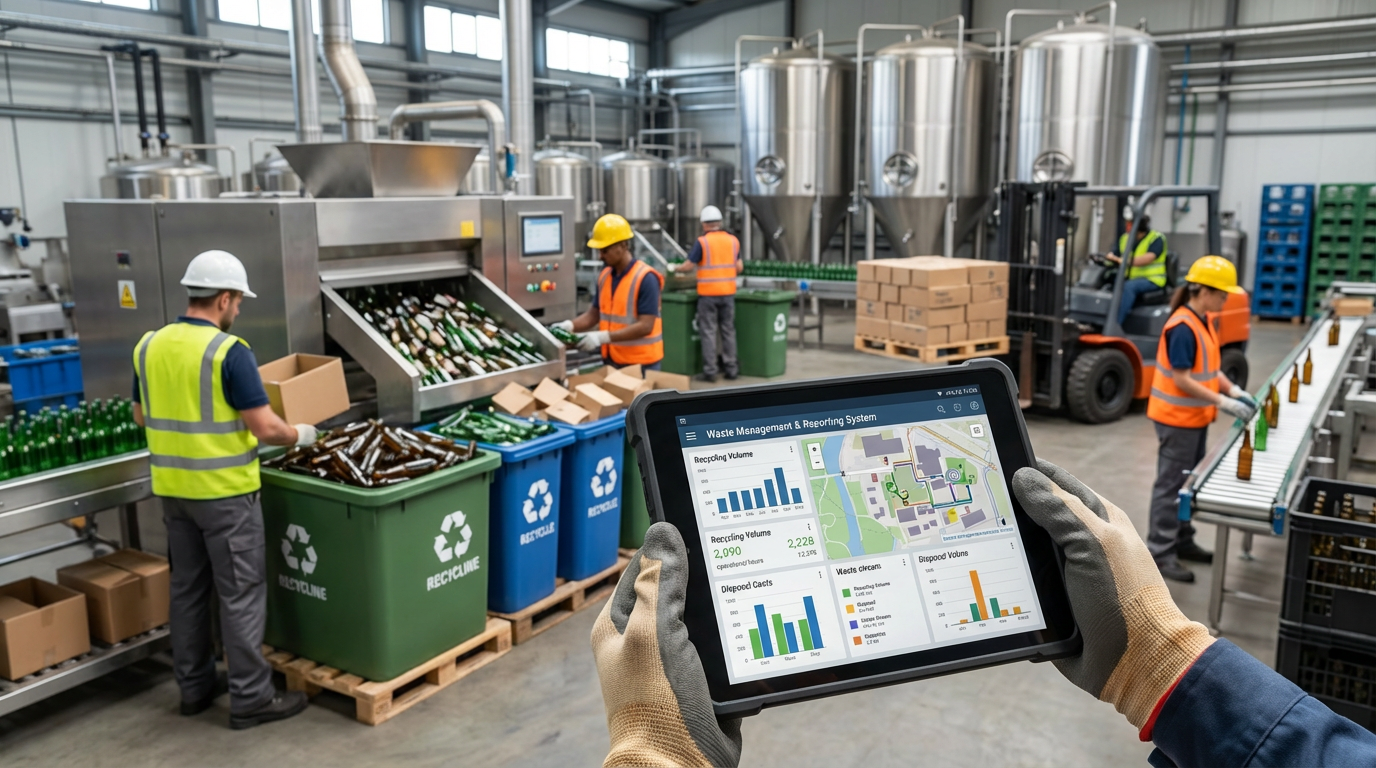
Capture and analyze waste data across all production stages to reduce inefficiencies. Detailed reporting helps teams identify cost-saving opportunities and meet environmental standards.
Key Capabilities:
Optimize beverage production from raw materials to packaging with unified controls, ensuring consistency, compliance, and operational visibility for all producers.
Leave your email below to start a new project journey with us.
Letโs shape the future of your business together.